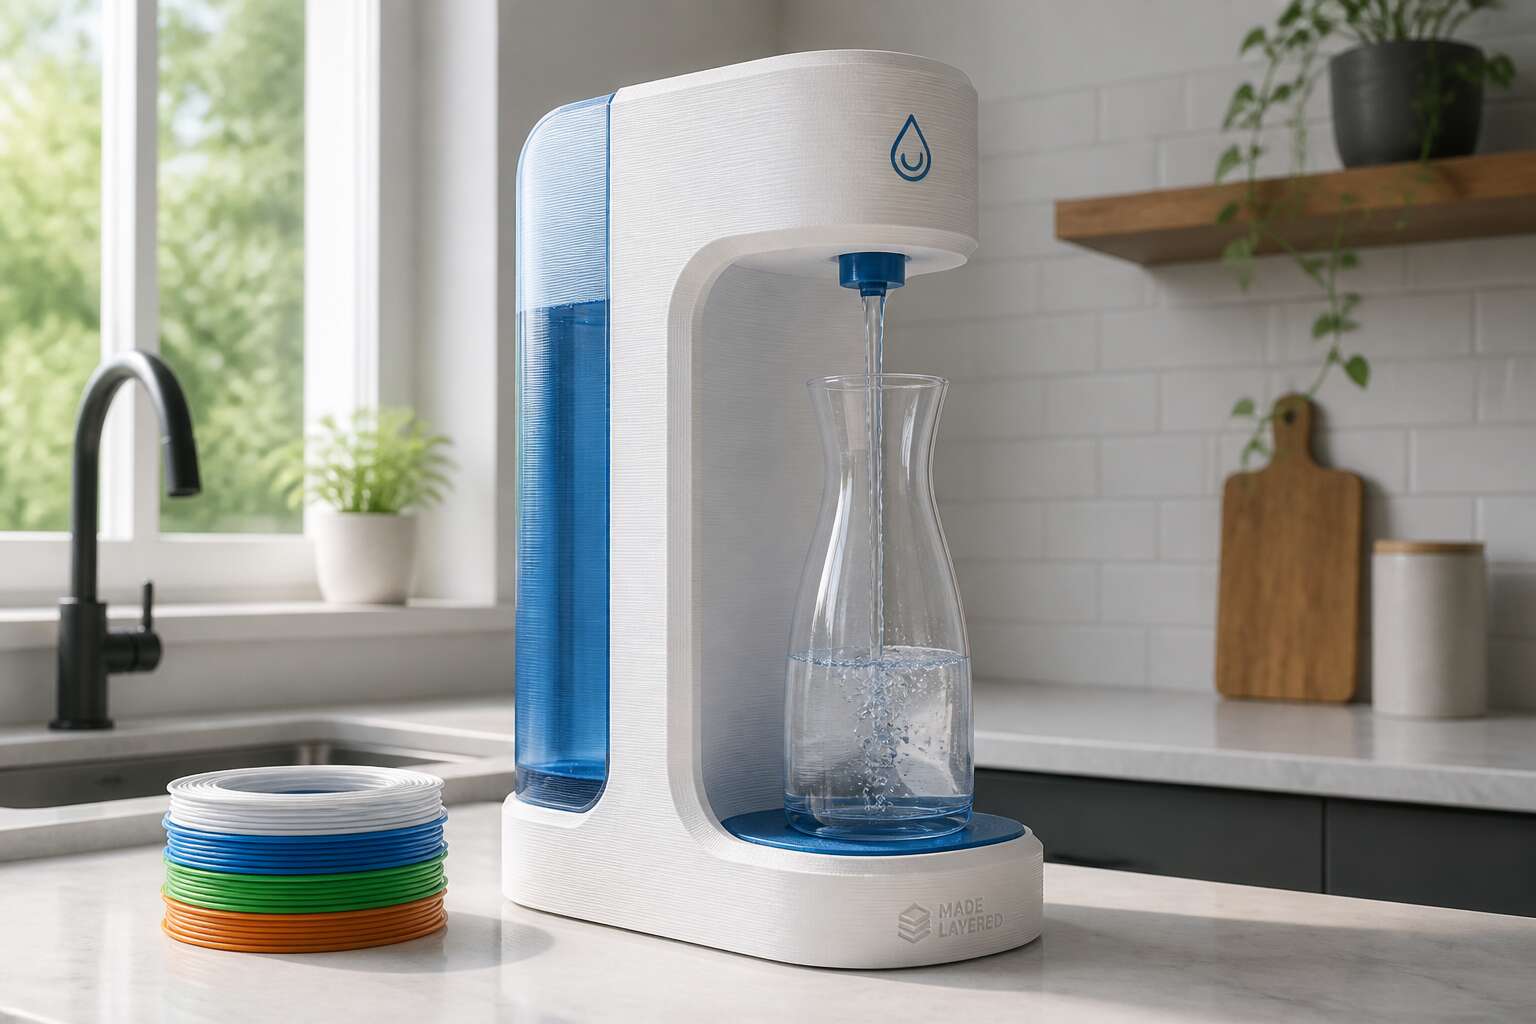
Why 3D Print a Water Dispenser?
Economic Benefits of DIY Fabrication
Consider the cost of a commercial water cooler. Now consider the price of a spool of filament. The gap is significant. A water dispenser 3d print lets you fabricate a functional unit at a fraction of retail. This is not about fragile prototypes. It is about durable, food-safe PETG.
- No retail markup
- No shipping or import fees
- No locked-in proprietary designs
DIY fabrication eliminates those costs. You pay for raw material and electricity. That is all! The economic benefit multiplies when you need multiple dispensers or custom brackets. Instead of buying proprietary parts, you produce them on demand. This matters in South Africa, where import duties and logistics inflate prices. A water dispenser 3d print turns a failed valve into a minor inconvenience, not a financial setback. Why pay for plastic moulding and transport when your printer sits idle? The savings start with the first print and compound with every replacement part you create.
Personalization and Design Freedom
The standard water dispenser is a stubborn piece of uniformity. Your countertop, your bottle size, your daily usage, none of it matters to a mass produced unit. A water dispenser 3d print changes that equation. You become the designer and engineer of a device shaped to your exact workflow.
Consider the possibilities. Adjust the spout height for a kettle or a sippy cup. Integrate a bracket for a drip tray that fits beneath your tap. Design a wall mounted version that clears a cramped kitchen counter. Retail models follow a generic blueprint; you do not.
- Custom spout angles for carafes
- Recessed storage for filters
- Mounting plates for load shedding prep
Hold a water dispenser 3d print in your hands and you hold a solution to your own constraints. That is the quiet power of design freedom.
The Rising Popularity of Custom Home Accessories
The home accessory market sells us convenience, but it rarely sells us meaning. Something is changing though. Across South Africa, more households are exploring what their own machines can build. The water dispenser 3d print has become a small emblem of this shift toward custom home accessories.
People want objects that carry a story. They want to know how a thing was made and how to remake it when it wears out. This desire drives the rising popularity of bespoke household items. It is a practical interest, not a nostalgic one.
- Design files shared freely by the global maker community
- Weekend workshops teaching basic fabrication skills
- A reliable alternative when retail supply chains stall
Each water dispenser 3d print, then, is less about dispensing water and more about reclaiming agency in a world of ready-made goods.
Addressing Environmental Sustainability
Every year, South Africans discard millions of plastic bottles and dispenser components. A water dispenser 3d print offers a different route. You fabricate the part from recyclable filament, often PLA or PETG, and when it cracks, you grind it down and print again. That loop keeps material out of landfills and reduces demand for virgin plastic production.
The sustainability argument also rests on transport emissions. Shipping a plastic dispenser from a factory overseas burns fuel at every stage. Printing locally, often in your own home, bypasses that supply chain entirely. The energy cost of one print is modest compared to the carbon footprint of global logistics.
- Recyclable thermoplastics reduce single use waste.
- Local production cuts freight emissions.
- Repair replaces replacement, extending product life.
Water scarcity in South Africa makes this water dispenser 3d print practical. A printed dispenser can be tailored to filter or store rainwater, supporting households that depend on collected water. This is sustainability that serves daily life, not an abstract ideal.
Fundamentals of 3D Printing for Liquid Contact Items
Choosing the Right Filament (PETG, PLA, Nylon)
The material science behind a functional water dispenser 3d print often dictates the difference between a showpiece and a daily driver. When you move from aesthetics to actual liquid conveyance, the polymer’s interaction with moisture becomes the primary design constraint. PLA, while wonderfully forgiving for prototyping, absorbs water and can degrade over time, compromising structural integrity where it matters most. PETG emerges as the pragmatic workhorse for this application, offering a superior balance of chemical resistance and dimensional stability.
Consider the thermal and physical demands placed on a spigot or reservoir base.
– PETG resists cracking under continuous pressure.
– It tolerates repeated cleaning with mild detergents.
– Its translucent properties allow for easy level monitoring.
– It does not impart a plastic taste to the water.
Nylon, though robust, is often overkill for static water pressure, but its low friction coefficient makes it ideal for internal valve mechanisms. The porous nature of Nylon, however, demands thorough sealing post-processing. For the South African climate, where water temperatures can fluctuate significantly, the slightly higher glass transition temperature of PETG offers peace of mind that PLA cannot. Prioritizing filament choice based on these specific mechanical properties ensures your water dispenser 3d print remains a sanitary and durable fixture. The safety of the water supply starts with the material touching it, so always verify the filament is free from heavy metal additives and is food-safe certified where possible.
Waterproofing and Sealing Techniques
Layer adhesion decides whether a water dispenser 3d print survives its first fill. An incomplete bond between perimeters creates a capillary path for moisture, and once water finds it, delamination follows. Maintain consistent nozzle distance, because micro-variances in extrusion width alter the weld strength between layers. Visual inspection of transparent walls is not sufficient. A controlled leak test remains the only honest validation method.
For a water dispenser 3d print, sealing starts with the reality that printed surfaces are porous. Vapor smoothing with a solvent bath can close micro-channels, though a thin coat of food-safe epoxy resin is the more reliable intervention.
- Acetate solvents attack PETG surfaces.
- Threaded joints require 100% silicone sealant.
- Annealing the part at 70°C relieves residual stress.
Internal stresses hide until pressurised. A 24-hour rest period after post-processing allows the polymer matrix to stabilise before meeting water.
Layer Adhesion and Leakage Prevention
A single drop finds its way through any gap wider than 0.2 mm. That is the threshold for a water dispenser 3d print. Layer adhesion determines whether a container holds or leaks. The core requirement is controlled extrusion pressure. I set my flow rate to 105%, pushing each layer into the previous one. Layer height should stay at 60% of nozzle diameter. Cooling fan stays off for the first five layers to promote welding. Check these fundamentals:
- Calibrate extrusion width to 110% of nozzle bore.
- Print outer perimeters before inner ones.
- Reduce speed to 25 mm/s for vertical walls.
Internal voids appear when these parameters drift. A water dispenser 3d print needs five perimeters, not two. Air pressure testing at 0.5 bar exposes weaknesses instantly. The polymer matrix relaxes over 24 hours.
Food-Safe Printing Considerations
The inside of a printed water vessel is rarely smooth, and that roughness carries consequences. Every water dispenser 3d print starts with material purity. I use only virgin PETG or polypropylene, never filament that has absorbed moisture. The fundamentals are wall thickness and infill density. A liquid vessel needs four perimeters with no gaps that could trap water.
Food-safe printing demands a clean hot end and fresh build surface. I avoid multi-color prints because pigment transitions create weak seams.
- Use a dedicated nozzle for food-grade projects
- Print at lower temperatures to prevent degradation
- Let the part cool slowly
These steps keep the water dispenser 3d print sound and free of contaminants. In a hot South African climate, a failed vessel is a health risk, plain and simple!
Structural Integrity and Stress Points
A water dispenser 3d print is a vessel that holds a heavy, moving burden. Every litre of water weighs one kilogram and presses outward against the walls with a force that grows with depth. The base bears the full weight, while the seams where perimeters meet become the first sites of failure.
The stress points live in the geometry. Sharp angles concentrate force, so I round every corner where the wall meets the floor. The spigot mount receives torque from every dispense, and a poorly anchored fitment will crack before the vessel does. For any water dispenser 3d print, the neck, the shoulders, and the transition zones are where layer lines split under load.
A cold dispenser in a hot Johannesburg room expands and contracts. That cycle, repeated daily, finds the weakest point and widens it over time!
Essential Tools, Materials, and Pre-Planning
Required Hardware and Fasteners
The difference between a dispenser that weeps and one that pours reliably often comes down to a single overlooked fastener. Before you commit to a water dispenser 3d print, measure your pump’s outlet and the reservoir neck with a digital caliper. Mismatched diameters cause more failures than any slicing issue.
Pre-planning the fastening strategy is equally critical. Brass heat-set inserts, stainless steel machine screws, and nylon washers resist corrosion in humid environments. For the plumbing, food-grade silicone tubing and hose barbs with a compatible inner diameter are non-negotiable.
A modest toolkit covers most builds:
– Digital calipers for verifying clearances
– Soldering iron with a heat-set insert tip
– Tap and die set for cleaning up threaded holes
– PTFE tape for sealing threaded connections
I have seen many water dispenser 3d print attempts stall because the components arrived without a clear assembly sequence. Lay out every part before printing. Verify that the pump, float valve, and tubing fit within the intended cavity.
Selection of Water Pumps or Valves
Pump selection is the moment when most water dispenser 3d print projects either find their rhythm or stall completely. A pump with too much flow creates turbulence and backpressure, while one with too little flow leaves you waiting. Measure the required lift and the desired pour rate, then consult the pump’s performance curve before writing a single line of G-code.
Pre-planning the valve type deserves equal attention. You have two basic paths:
- Float valves for passive, mechanical level control in gravity-fed reservoirs.
- Solenoid valves for active, electronic dispensing when paired with a microcontroller.
Match the valve’s thread size to the pump outlet before printing the mounting bracket. Hard water can clog a solenoid over time, so position service ports where you can reach them. Keep a multimeter and a bottle brush nearby. The multimeter verifies current draw against the power supply, and the brush cleans the reservoir’s interior before assembly. Both take minutes and save hours later.
Estimating Print Time and Volume
Essential tools rarely appear in glossy renders, yet they determine whether a water dispenser 3d print survives contact with water. The short list:
- Digital calipers for measuring wall thickness
- A filament scale to catch mid-print shortages
- A deburring tool for clearing internal water channels
Calipers confirm shrinkage behavior. The scale prevents abandoned builds. The deburring tool clears narrow passages that clog with stray wisps of plastic.
Estimating print time and volume demands more than slicer software. The slicer calculates extrusion distance, but not the minutes lost to travel moves and retractions. A water dispenser 3d print with internal baffles consumes fifteen hours at 0.16 mm layers. The same body at 0.28 mm layers takes nine hours. Thicker layers leave microscopic valleys that sealing compounds must fill. Thin layers merge into a smoother surface that holds up to water pressure. Weigh the filament spool first. Add fifteen percent to the slicer estimate. The real world always asks for more.
A Detailed Step-by-Step Print and Assembly Guide
Preparing the 3D Model and Slicer Settings
A single misaligned support can waste 14 hours of print time. Before exporting your STL file, inspect the model for overhangs and thin walls. Orient the body so the nozzle and valve ports face upward.
In your slicer, set the layer height to 0.2 mm. Use 20% infill with a gyroid pattern for the base, but switch to 100% solid layers around the pump mounting flange. For a water dispenser 3d print, enable supports only for the spout’s internal channel, then adjust the density to 10%.
- Set the print temperature to your filament’s extrusion curve.
- Disable the cooling fan for the first three layers.
- Verify retraction distance to avoid stringing in the reservoir.
After slicing, simulate the toolpath. A successful water dispenser 3d print relies on precise internal geometry, so any bridging defect compromises the flow path. Use a 0.4 mm nozzle with 0.3 mm extrusion width.
Bed Adhesion and Print Orientation
Half of the failed prints in my Johannesburg workshop share one cause: the first layer never held. The rest failed through haste, but this particular failure arrives with patience. A water dispenser 3d print either grips the plate within the opening seconds, or it spends hours lifting and warping before detaching.
Orient the reservoir’s flat base directly onto the build surface. The spout and valve ports face upward, away from the bed. This placement keeps support material out of the interior channel.
- Clean the plate with isopropyl alcohol before each attempt.
- Add a 5 mm brim around the base footprint.
- Hold the bed temperature at 65°C for PETG.
The nozzle must sit at a precise height above the plate. A water dispenser 3d print demands that the first strand be pressed flat, not dragged across the surface. Set the height with a feeler gauge and trust the measurement.
Removing Supports and Post-Processing
A water dispenser 3d print completes its marathon with a silent hum of the cooling fans. The moment the print head retracts for the final time, a new phase begins. You will spend as much time finishing this piece as you did printing it. The supports scream for your attention, especially those fragile columns that protected the spout’s inner curve during fabrication. Patience serves you well here, as the plastic rewards a gentle hand over brute force.
Begin by removing the print from the bed. Use a flexible spatula, sliding it beneath the brim that secured the base. Once free, switch to a pair of flush cutters. Snip away the brim in small, deliberate sections. Avoid twisting or prying, as the reservoir walls may flex and crack under sudden pressure.
For the support structures, work from the outside in. Use the following tools in this order:
– Flush cutters to remove larger, exterior supports.
– A needle-nose pliers set to extract deeper sections within the valve cavity.
– A small rotary tool with a sanding drum if supports resisted removal.
The interior channel is where most operators ruin their project. Abrasive tools can dig into the wall and create a weak point that will fail later. Use the pliers to pull away the support material in small pieces, working toward the center of the reservoir. Once the channel is clear, run a soft filament brush through the opening to remove plastic dust from the sealing surface.
After the supports yield, post-processing begins. Sand the flat base with 200-grit paper to remove the brim remnants and ensure a level surface. The seams where print layers meet can be smoothed with a warm soldering iron set to 250°C. Drag the tip lightly over the layer lines to melt them into a uniform finish. The water dispenser 3d print will also benefit from extra attention to the valve port threads, if your design included them. Clean the threads with a fine pick to ensure a snug fit for your hardware.
You must also verify the wall thickness of the reservoir. Use calipers on the side walls near the base, where the layer lines are most visible. A measurement below 1.2 mm suggests over-extrusion during the print. The wall may flex, so reprint with corrected flow settings before assembly. When you finish the cleaning and sanding, run water through the dispenser manually to confirm the channel is open and the spout releases a steady stream. This final check saves you from a difficult disassembly later.
A finished water dispenser 3d print is more than a plastic shell. It is a sequence of disciplined choices, from the first layer height to the last sanding pass. Each action contributes to the vessel’s integrity. Appreciate the quiet satisfaction of a part that holds water without a single drop of leakage, knowing your hands measured every step along the way.
Assembly of Connection Ports and Dispensing Nozzle
Attaching the nozzle to your water dispenser 3d print is where hand cramps meet engineering pride. I have watched makers torque fittings like they were loosening lug nuts. Stop. The connection port deserves the same precision you gave the reservoir. Clean the threads with a fine pick, wrap PTFE tape clockwise around the fitting, then thread it by hand until you feel resistance. A quarter turn with a wrench is plenty, overtightening cracks the port flange.
The dispensing nozzle needs heat-set inserts instead of self-tapping screws. Heat your soldering iron to 260°C, press the insert straight in, and hold for five seconds. Once seated, add a soft silicone washer between the nozzle and the housing.
- Check that the barbed fitting seats completely before snugging the collar.
- Run warm water through the system first to expose any micro-cracks near the port.
South African municipal pressure will punish a lazy seal. A pressure-reducing valve on the inlet keeps your water dispenser 3d print alive when the mains surge.
Testing for Leaks and Flow Rate
Testing begins when the last fitting is snug. I fill the reservoir with warm water and watch every joint closely. Micro-cracks near the ports reveal themselves as beads of moisture within minutes. The pressure-reducing valve should be set to 2 bar before you open the mains supply. A water dispenser 3d print only survives this stage if the seals were honest.
- Inspect the reservoir seam and the port flanges.
- Run the pump at half speed and listen for air hiss.
- Feel the silicone washer at the nozzle for dampness.
Flow rate reveals the real situation. My water dispenser 3d print with a 12V diaphragm pump delivers roughly 2.5 litres per minute through 6mm tubing. If you see less, check the PTFE tape on the fittings and the heat-set insert seating. South African municipal pressure can spike to 6 bar, so never test without the reducer in place. Warm water exposes cracks that cold water hides. Let it run for ten minutes before you call the job done!
Safety, Troubleshooting, and Maintenance
Common Printing Defects to Avoid
Most leaks start with a missed detail. A water dispenser 3d print demands respect for electricity and moisture. Keep pump wiring separated from wet surfaces. Use a residual current device on the outlet. Moisture creeps into unsealed seams. Trust me, it finds every gap!
Start with the nozzle. A partial clog produces a weak stream, not a leak. Check tubing for kinks. If flow pulses, purge trapped air slowly. For your water dispenser 3d printing project, inspect the valve seat regularly. Dust creates a permanent drip.
- Warping at the base from a cold draft
- Stringing between the nozzle and tank wall, which blocks the outlet
- Under-extrusion near the bottom bracket, which weakens mounting points
Maintenance is simple. Wipe the exterior weekly. Flush the internal lines monthly. Replace the tubing every six months. A tiny crack in the bracket grows after each refill. Tighten screws gently. Plastic threads strip easily.
Ensuring Hygiene and Preventing Bacterial Growth
Biofilm forms within 24 hours on any damp surface. That shapes safety for a water dispenser 3d print. Keep the electrical housing sealed and elevated. A drop of condensation can bridge the circuit. Given load shedding, expect power surges. Use a residual current device and inspect the cord monthly.
Troubleshooting starts with sound. A weak stream often means a clogged nozzle. A dull hum indicates pump cavitation. Check the filter housing for trapped particles. I have seen flow drop from a blocked air vent, so open the release valve slowly.
Maintenance ensures hygiene and prevents bacterial growth. The reservoir is the highest risk zone.
- Flush the tank with warm water and vinegar weekly.
- Sanitize the dispensing tip after each refill.
- Air dry all parts before reassembly.
Pay attention to the rubber gasket. Replace it every three months. Position your water dispenser 3d print near a bright window, but away from direct heat.
Troubleshooting Leaks and Cracks
Safety with a water dispenser 3d print means respecting the difference between a clever project and a conductive puddle. A cracked reservoir will flood your kitchen faster than a Joburg summer storm. Inspect the layer lines for micro-fractures, especially near the outlet port where stress concentrates every time you yank the bottle out. I once ignored a faint creaking sound. The next morning, my shoes made a squelching noise.
Troubleshooting leaks and cracks demands patience, not panic. A slow weep at the base usually means a loose insert, so grab the epoxy. A hairline split along the layer seam needs a soldering iron, or a complete reprint if the part carries water pressure.
- Check the underside of the nozzle for stress whitening.
- Dry fit cracked parts before touching the electronics.
- Keep spare gaskets away from sunlight to prevent perishing.
Maintenance for a water dispenser 3d print is about catching a hiss before it becomes a hose. That sound is air entering a gap, and a gap means growing damp patches.
Repairing and Extending the Product Lifespan
Safety starts with the assumption that every water dispenser 3d print is a potential electrical accident. The pump motor draws current near the reservoir. I keep the electronics in a separate compartment, sealed against condensation. Any splash that finds its way to the terminals is a short circuit waiting for load shedding to expose it.
Troubleshooting beyond cracks involves the peristaltic pump stalling. A blocked inlet line produces a high pitched whine.
- Check the tubing for kinks.
- Purge air from the pump head.
- Verify the gear ratio hasn’t slipped.
That whine is the system telling you where the resistance lives.
Maintenance and repair extend the lifespan of your unit. Replace silicone gaskets every six months. Reapply food safe waterproofing to the nozzle flange. Sand down any rough edges before they become bacterial colonies.

0 Comments